

If you’re reading this post, chances are you want to know how machine vision imaging can help your business. Today I’m discussing 3 of those ways. So read on to find out machine vision imaging can help your business.
*This is a partnered post
How Machine Vision Imaging can Help Your Business
In case you’re not familiar with Machine Vision Imaging, and how it works, I’ll start by explaining. In simple terms, Machine Vision is technology which provides imaging-based, automatic inspection and analysis. It is often used for things like automatic inspection, process control, and robot guidance.
Machine Vision Imaging can help your business to make manufacturing processes more efficient, increase productivity, and reduce waste. It is also often used to make recycling processes more efficient.
Using Machine Vision Imaging to Improve Quality Control Processes
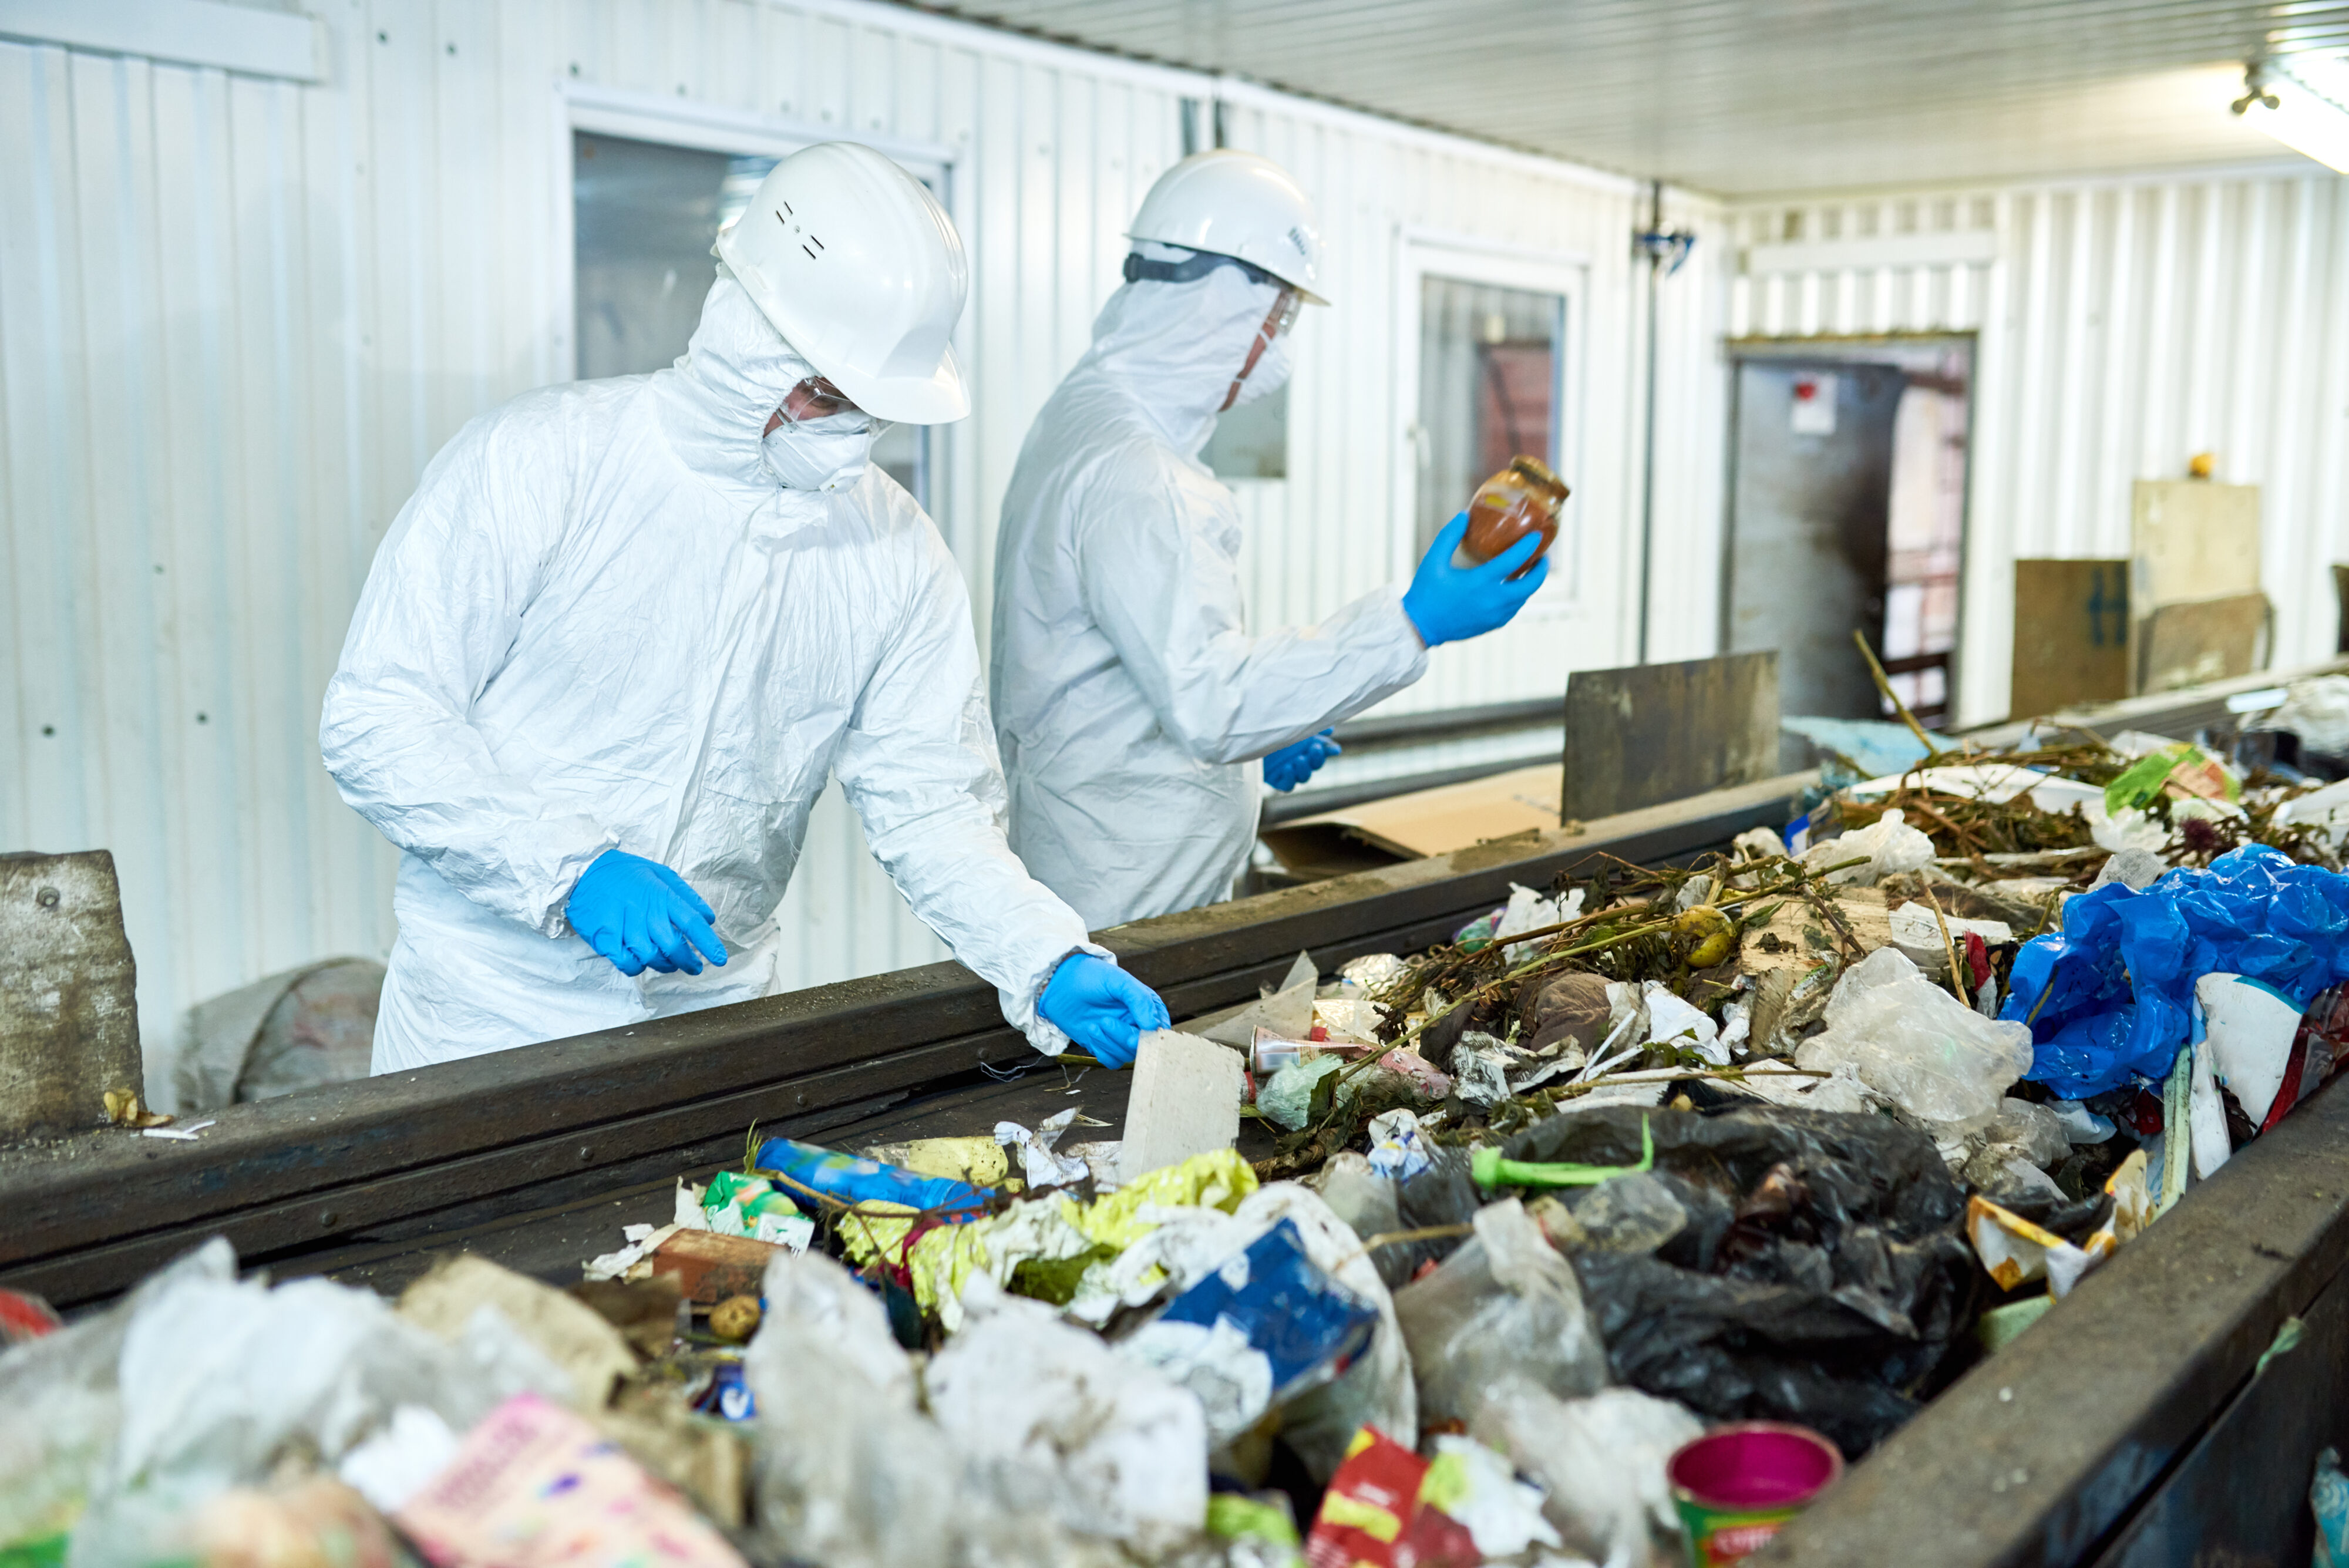
One of the biggest risks to employees in a recycling plant is getting injured during the sorting process. Whether that’s getting cut or scratched by sharp edges, or risking contamination when they come into contact with used syringes or such like.
Imagine being able to use Infra-Red to make sure there’s nothing warm in the midst of a filled Dumpster or Skip. Add to that, the ability to automatically sort recyclable items from general waste. That’s just one of the ways machine vision technology can help your business.
Machine Vision Imaging Can Improve Health and Safety
Investing in machine vision Technology can mean better Health and Safety records. There are plenty of ways machine vision imaging can help your business, from a safety perspective. The system could scan your building site in real-time to make sure everyone is wearing High-Vis vests, hard hats and boots.
It could also ensure scaffolding doesn’t get over-crowded. The system scans individuals to ensure they are adhering to your pre-set health and safety criteria. If they aren’t, the system will alert the necessary people. This can mean less in-person safety inspections are required and a better health and safety record for your business.
Using Machine Vision Technology for Quality Control
Quality control is often a time-consuming and costly part of the manufacturing process. One of the ways machine vision imaging can help your business is by making sure each item meets a pre-set quality control criteria.
Not only does this get rid of the risk of human error, but it also means you’ll be made aware as soon as something goes wrong on the production line. Whether that’s a bottle containing less liquid, or the label being off-centre, machine vision technology has the ability to pick up on the issue immediately.
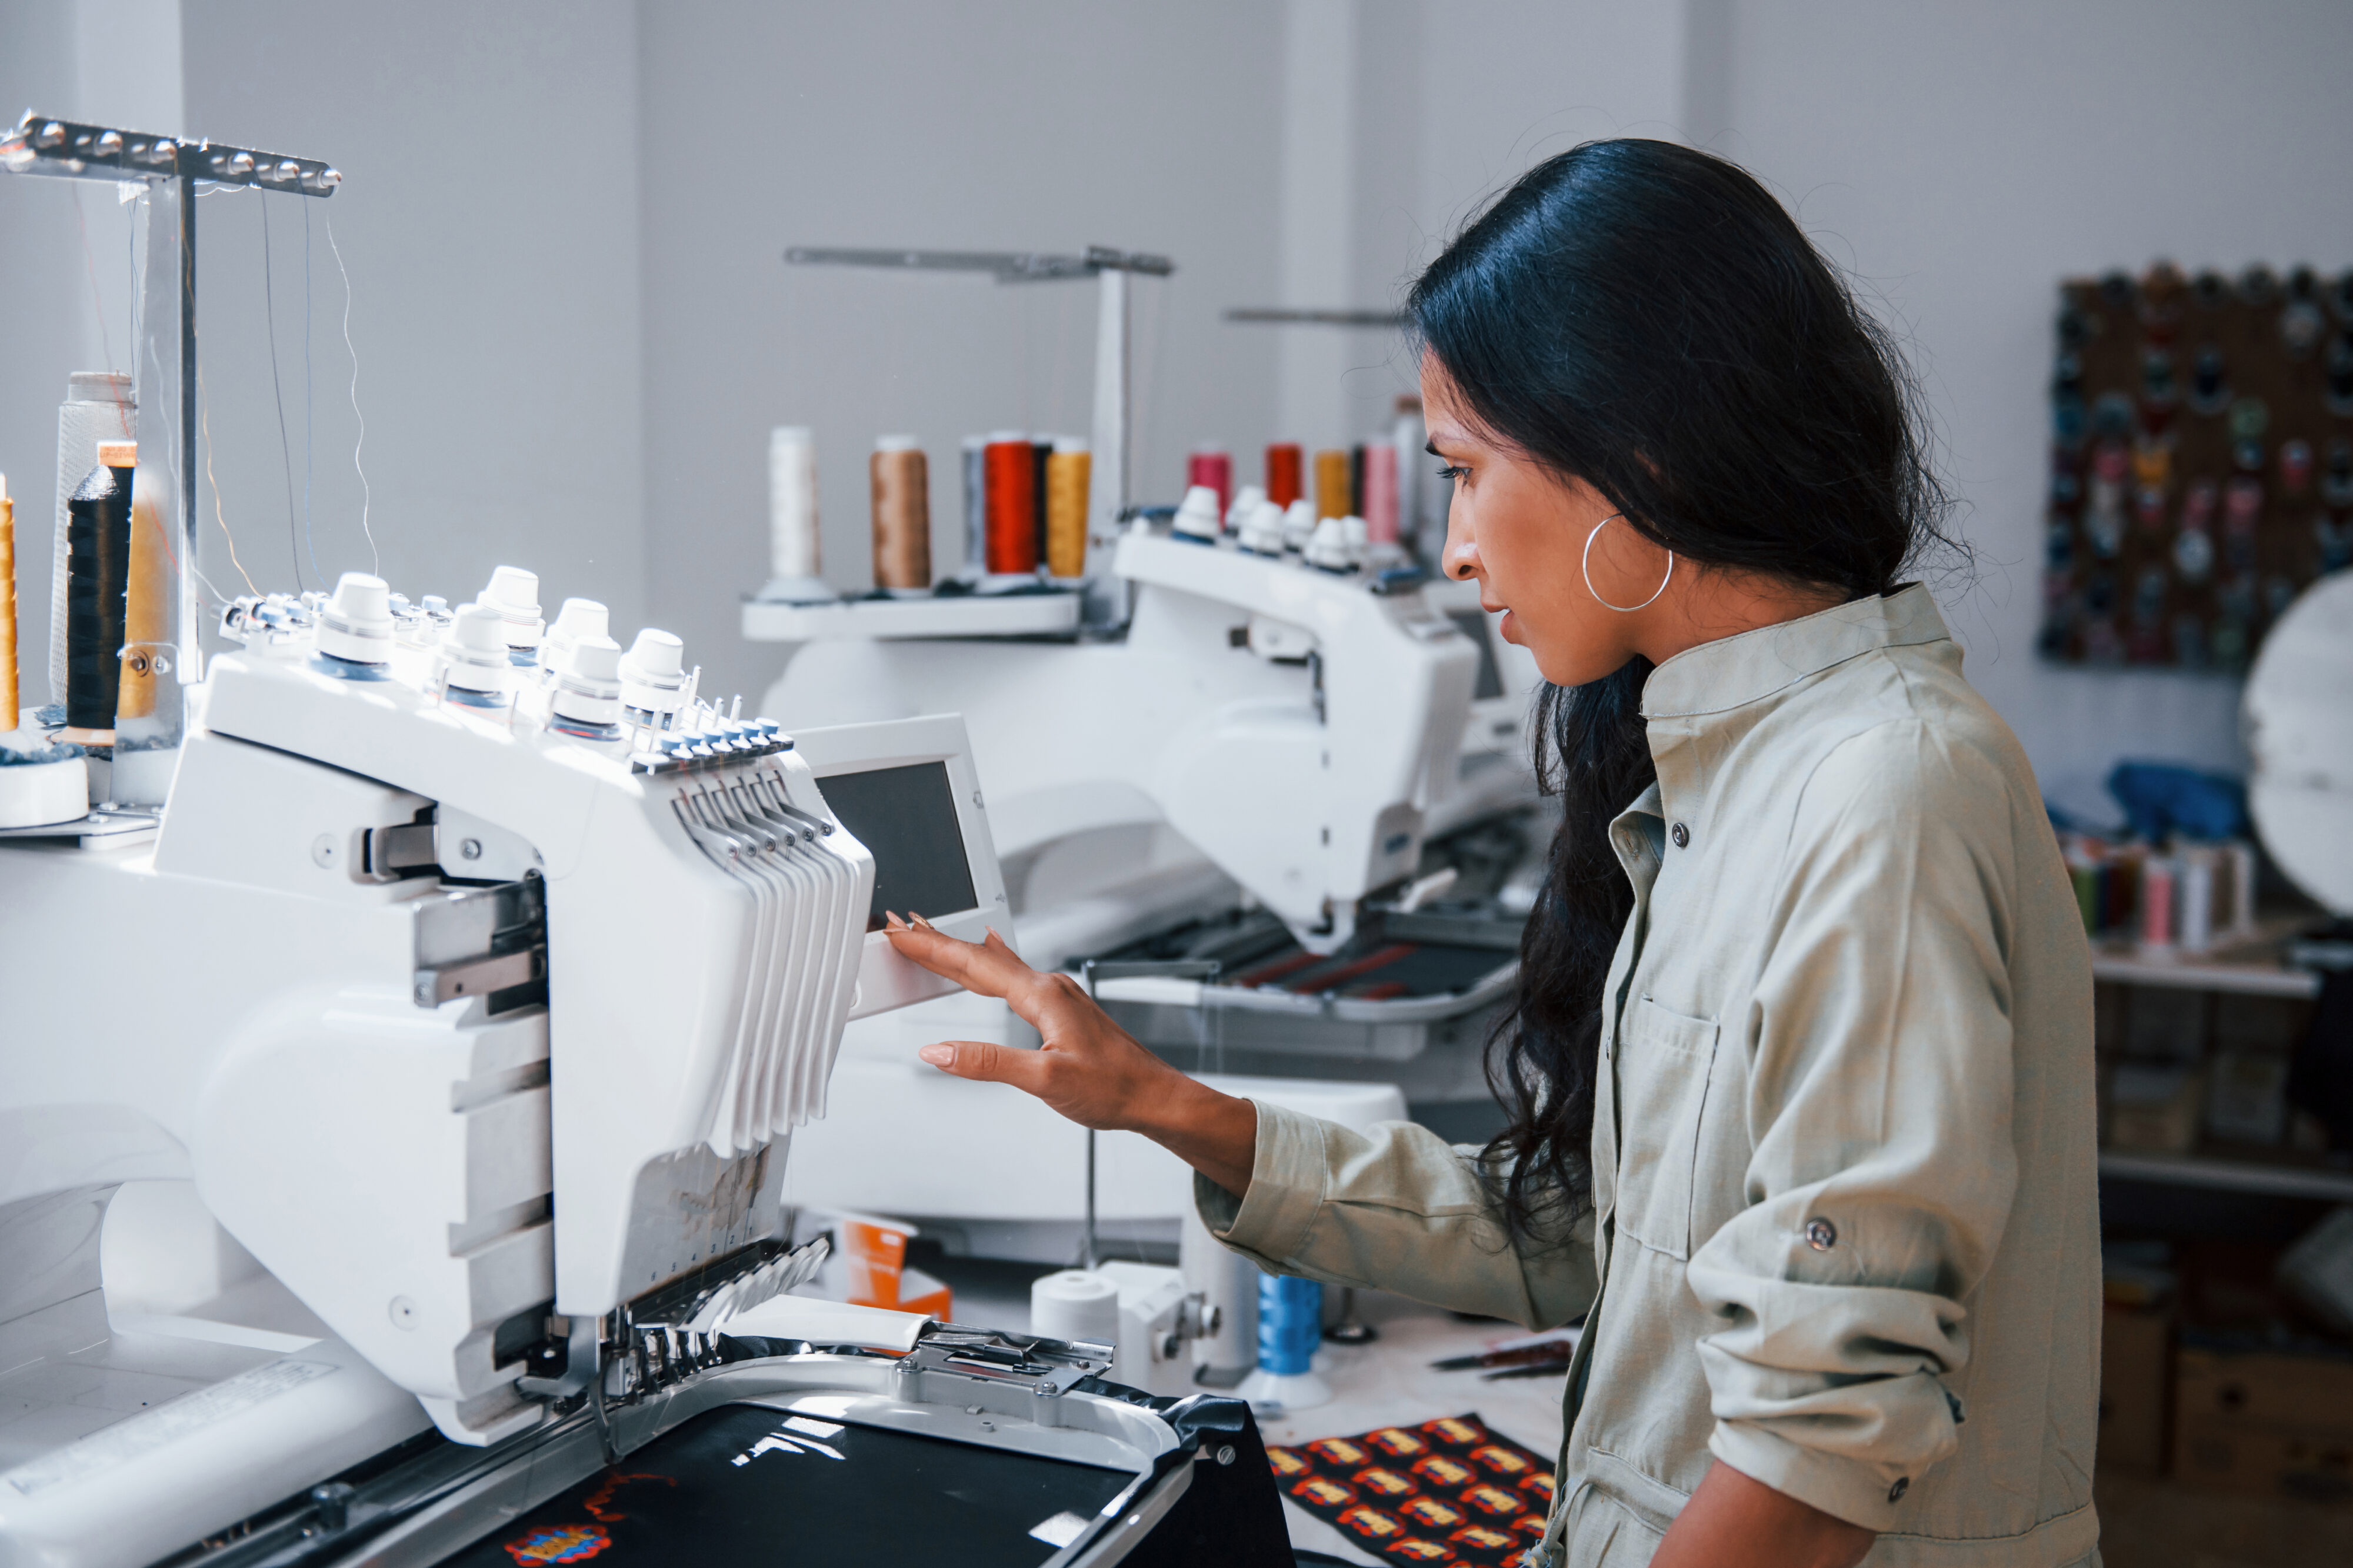
Machine vision imaging can help your business in plenty of other ways, too. If your business involves embroidery, the technology can spot issues with clarity, dropped stitches or colour issues, amongst other things.
Using Machine Vision to Sort Products
Machine vision imaging can help your business in many ways. One of the most popular uses is sorting products. Imagine if your online retail business receives thousands of returns a week. Being able to use this technology to sort faulty returns from items which were just unsuitable, and can be re-sold is a great initiative.
You can even take this one step further, and use it to separate your stock deliveries. The technology can scan all of the products which arrive, and allow you to ensure they are placed in the correct area of your warehouse.
You could even use it to sort individual lines by colour or size, as well. This information could be uploaded to your website automatically, so your stock levels update in real-time. This is a great way to help ensure business success.
So there you have it – just 4 of the ways your business could be helped by Machine Vision Imaging. Does it sound right for your business?
